Knowledge Center
Method Development for a CCI Test Using Headspace Gas Ingress
Not every loss of container closure integrity (CCI) is visible. A microscopic crack can hide beneath the crimp, and a container that lost closure only temporarily can look sealed. Headspace gas ingress testing finds these failures by exposing sealed containers to a tracer gas and measuring, non-destructively, whether it enters the headspace. This article follows headspace gas ingress method development for a 15R vial, from tracer gas choice to positive control design.
The right method depends on your container closure system, life cycle stage and required throughput. USP <1207> describes headspace analysis as a deterministic test, preferred over probabilistic methods such as blue dye ingress and microbial challenge testing. See also our dedicated page on CCI test method validation and development.
Choosing a tracer gas: CO₂ or headspace oxygen
In a product with modified headspace such as a nitrogen overlay, a leak lets air in, and rising headspace oxygen signals a loss of CCI. A container with an ambient air headspace gives no such signal: a leak does not change its gas composition. That is why carbon dioxide is used as a tracer gas. Very little CO₂ is naturally present in the atmosphere, so even a small increase can mark an integrity failure.
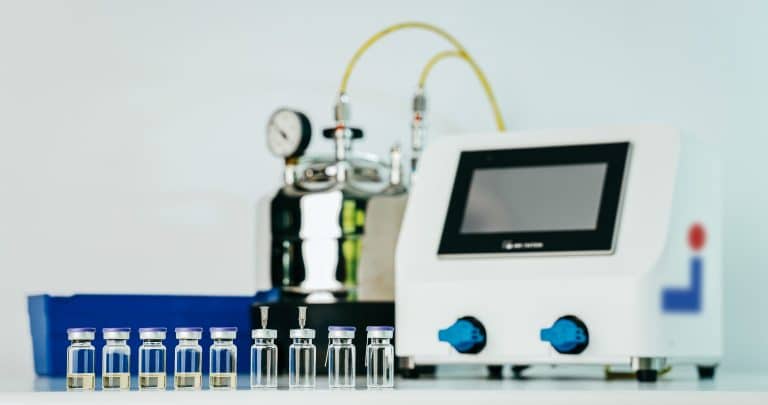
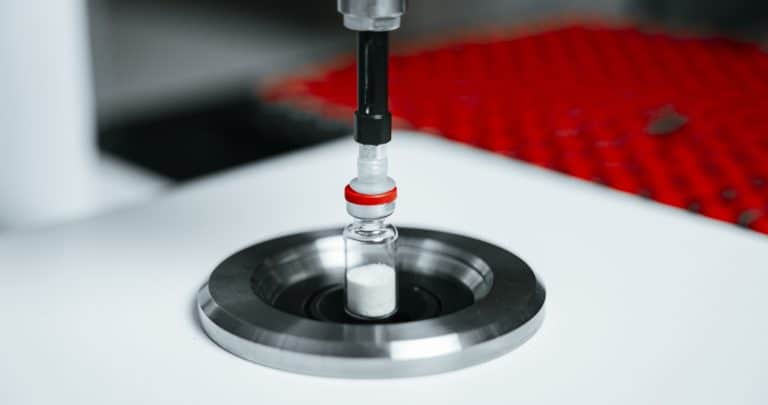
To accelerate ingress, samples are pre-conditioned in a CCI test vessel before measurement. Conditioning cycles can include pulling an initial vacuum and backfilling with CO₂, over pressurizing with CO₂, or both. Headspace CO₂ is then measured with a headspace carbon dioxide analyzer. The concept is similar to blue dye ingress, but the result is deterministic, rapid, non-destructive and analytical.
Designing positive controls: defined leak path or realistic defect
Before selecting positive controls, define the scope of your method:
- In which life cycle stage will the test be used?
- Which defect types carry the highest risk of occurring?
- What leak detection sensitivity is required?
- Can the product formulation interfere with the CCI test?
- Is the package or product affected by the test method?
Positive and negative controls then confirm that the method separates leaking from non-leaking packages. Choosing a positive control is a trade-off between a defined leak path and a realistic defect. Laser-drilled defects offer a relatively well-defined leak path. Micro-capillaries, micro-pipettes and needle punctures have a defined leak path, but are unlikely to occur in real packages.
Microwires and micro-cracks sit at the other end. A micron-sized wire between vial neck and stopper simulates a fibre or hair stuck in the sealing area, which is a realistic defect. Its leak path, however, is not well defined and can vary with sample preparation, stopper elasticity and crimping compression. The full article compares all six control types.
What this study shows
The study used 15R vials with laser-drilled and microwire positive controls in three fill states: empty, 5 mL phosphate buffered saline (PBS), and 5 mL bovine serum albumin (BSA) in PBS at 1 mg/mL. Laser-drilled defects were positioned underneath the liquid fill, and microwire vials were inverted three times so the fill reached the defect. After a baseline measurement (T0), samples underwent a 30-minute CO₂ overpressure cycle in the test vessel, followed by a second measurement (T1).
Every empty laser-drilled control was detected. For laser-drilled control vials with a liquid fill, the results depend on the location and size of the defect. Liquids, and protein solutions in particular, tend to clog defect sites, and the tracer gas must first overcome surface tension.
These defect sizes do not represent the limit of detection. Overpressure and hold time can be adjusted to target the desired defect size for any product-package configuration.
The microwire sets showed larger sample-to-sample variation, because the compressed rubber stopper flows and partially seals around the wire. That variation illustrates how realistic microwire defects are. See also correlating headspace gas ingress testing to helium leak rates.
From method development to validation
The parameters set during development become the defined test method for validation. Validation should demonstrate that the method differentiates leaking from non-leaking containers and verify the Limit of Detection (LOD), with the test performed multiple times by multiple operators.
Because the test is non-destructive and analytical, parameters can be optimized per product configuration. Read more about CCI test method validation and development, or see the approach applied to a different container in our case study on CCI test method validation for prefilled syringes.